Fabricating ACM Panels: A Shop Guide From Sheet to Installed Cassette
Cut, groove, fold, rivet, hang. The whole sequence for a composite cassette, and where each step goes wrong.
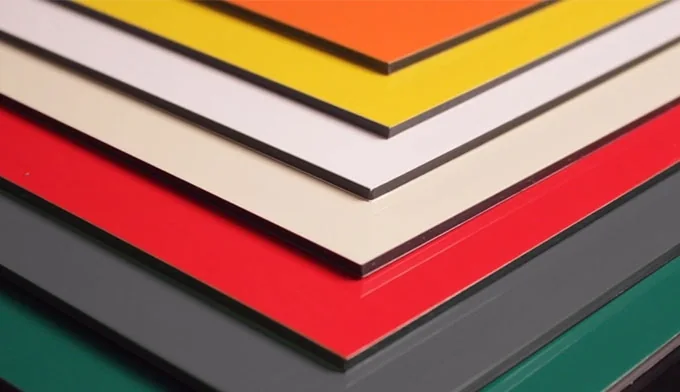
A composite cassette looks like a solid metal box. It is a flat sheet that was cut, grooved on the back, folded, and fixed at the corners. Every shopfront, column cover and soffit panel you have looked at was made that way, and the difference between a good one and a bad one is almost entirely in the first two steps.
This is the whole sequence, in the order a shop actually does it.
1. Decide the finished size, then work backwards
A cassette is described by its face dimensions and its return depth. The flat blank you cut is the face plus one return on each folded side, plus nothing else — the fold consumes no material, because the V-groove has already removed it.
So a 600 by 400 face with 25 mm returns on all four sides is a blank of 650 by 450. Write the blank size on the sheet before you cut, not the face size. More panels are scrapped by cutting the face size and discovering the returns have nowhere to come from than by any other single mistake.
2. Square one edge, and never reference anything else
Take a thin cut off one long edge of the sheet and mark it. That edge is your only datum for the whole job. Every subsequent cut references it, directly or through a stop — never through another cut edge, because a cut edge carries whatever error the cut that made it had, and by the fourth part the error has compounded four times.
This is also where a continuous bed earns its money. On a 157 in (4,000 mm) frame the sheet is carried for its whole length and the offcut never drops, so the last part of the cut does not close on the blade and taper.
3. Cut the blanks to size
Batch by length. Set the stop once, cut every blank that shares that length, then move the stop. On a job of twenty identical cassettes that is one setting operation instead of twenty, and the twenty panels are copies of the same physical distance rather than twenty readings of the same number.
Keep the protective film on both faces. It is the cheapest edge protection there is, and on a coated composite the film is also the only thing standing between your bench and a scratch that will be visible from the pavement.
4. Groove the back
Mark the good face before the sheet goes on the bed, and keep the marked face down. The groove goes in the back — the face that disappears after the fold.
A 90 degree V leaves the panel free to close to a square corner and stop there: the geometry sets the angle, not your hands. What you are controlling is depth. Leave the face skin plus a thin film of core as a hinge — too much and the panel will not fold without a stress line showing through; too little and the hinge tears, sometimes months later on a cold morning.
Set the depth on an offcut of the same sheet, every time the sheet changes. Core formulations differ between suppliers and between batches, and a setting that was right last month is a guess this month. Fold the test piece all the way and open it again: a clean fold that opens without whitening means the hinge is right.
The groove must also be straight over the whole panel. A groove that wanders by a millimetre over 10 ft gives a corner that is visibly not parallel to the edge, and on a run of twenty cassettes it is the one everybody looks at. That is the case for a guided carriage on a profile rail rather than a hand-held router on a clamped straightedge.
5. Fold
Fold against something straight so the bend starts along the whole line at once. Freehand folding puts the bend a few millimetres off the groove in places, which reads as a soft, wavy corner. Fold the two short sides first, then the long ones, so the long returns close over the short ones.
6. The corner
Where two returns meet you have a choice, and it is a visual one:
- Lapped and riveted. Fastest, strongest, and the rivet head is visible from the side. Standard for soffits and for anything above eye level.
- Mitred and bonded. Invisible from any angle, slower, and it wants a structural adhesive and a jig to hold the angle while it cures. Standard for anything at eye level on a shopfront.
- Corner cleat. An internal angle riveted to both returns. Adds stiffness to a large panel and is hidden.
Decide this before you cut, because a mitred corner needs the return corners notched and a lapped one does not.
7. Stiffeners, if the panel is large
A flat composite face over about a metre will show a slight oil-canning under raking light. The cure is a stiffener bonded to the back — an aluminium extrusion or a folded strip — not a thicker sheet. Bond it with a flexible structural adhesive, never a rigid one: the panel and the stiffener expand at different rates, and a rigid bond telegraphs that difference straight through to the face.
8. Hanging
Composite moves. A 3 m panel can change length by a couple of millimetres between a winter morning and a summer afternoon, so every fixing except one has to allow it to. One fixed point, the rest on slotted holes or a rail system, and no fixing pulled up tight enough to pin the panel.
Where each step tends to fail
| Step | What goes wrong | What prevents it |
|---|---|---|
| Sizing | Face size cut instead of blank size | Write the blank size on the sheet |
| Squaring | Referencing a cut edge | One marked datum for the whole job |
| Cutting | Taper at the end of the cut | Continuous support; offcut stays on the bed |
| Grooving | Hinge too thin or too thick | Test on an offcut of the same sheet |
| Grooving | Groove not parallel to the edge | Guided carriage on a rail, not a clamped straightedge |
| Folding | Wavy corner | Fold against a straight edge, short sides first |
| Corners | Mitre gaps | Decide the corner before cutting; notch the returns |
| Installation | Oil-canning, pulled fixings | Stiffeners; one fixed point, the rest floating |
Where to read the numbers
The frame, bed and carriage specification is on the specification page, and the machine page walks through the four moves a job takes. If you are weighing this against the tools already on your floor, the comparison page says where each one wins. For a delivered figure, use the quote form.
Comments 0
Be the first to comment.